Product Description
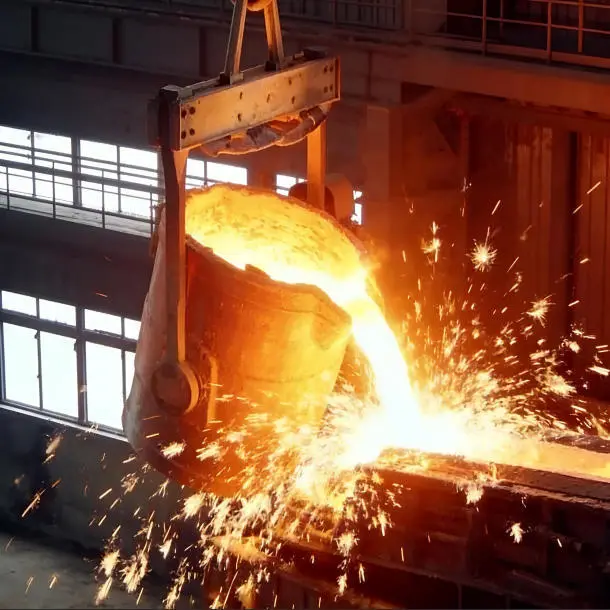
SAF Casting System Hot Metal Ladle / Casting Machine / Ingot Machine
I. Overview:
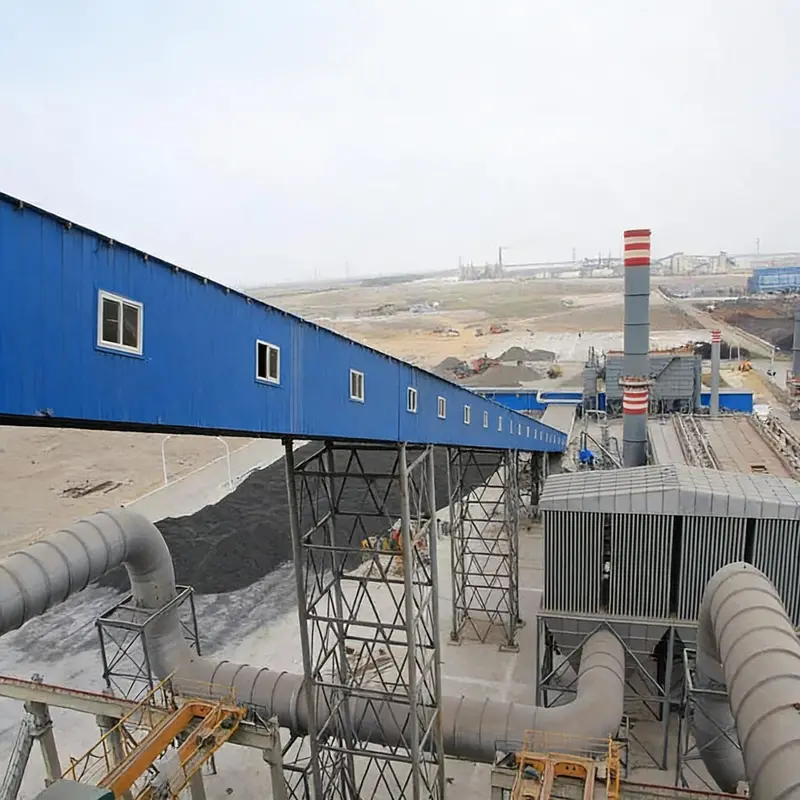
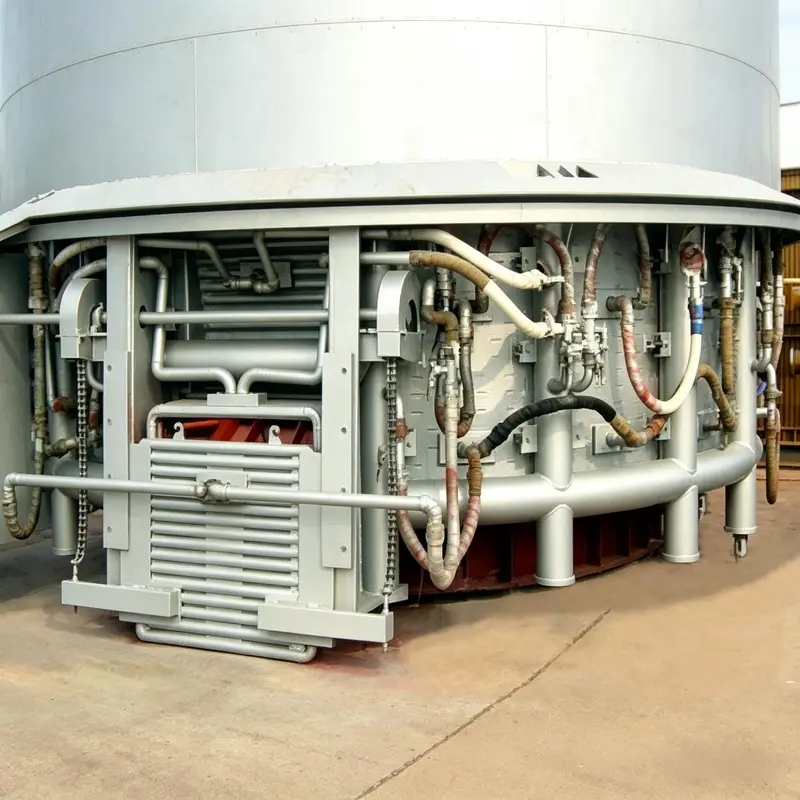
The casting system is a complete set of equipment for pouring liquid metal into molds for solidification, serving as the core part of metallurgical production.
II. Permanent Mold Casting System
Permanent mold casting, also known as hard mold casting, is a process where liquid metal is poured into reusable metal molds to obtain castings. This method features high mold reuse times (hundreds to thousands) and high production efficiency.
Key Process Parameters
| Parameter | Requirement |
|---|
| Mold Preheating Temperature | ≥150℃ |
| Mold Material | Mainly cast iron, aluminum alloy cavity can be anodized |
| Coating Requirement | Spray refractory coating to adjust cooling rate |
| Casting Weight Limitation | Not too large |
| Casting Shape | Mainly simple shapes |
III. Continuous Casting System
Continuous casting is a production process that continuously pours high-temperature molten steel into castings with specific cross-sectional shapes and dimensions, and is the core technology of modern steel industry.
Typical Continuous Casting Machine (CCM) Technical Parameters
| Parameter | Range |
|---|
| Annual Production Capacity | Slab: 2-2.5 million t/year
Bloom: 0.8-1 million t/year
Billet: 0.6-0.8 million t/year |
| Operating Rate | 80-90% |
| Casting Speed | Slab: 1.2-1.8 m/min (max 3.0)
Billet: 2.5-3.5 m/min |
| Sequence Casting | Average 4-6 heats, max 329 heats |
| Radius | 11-17 m (max 18.5 m) |
IV. Ingot Casting System
Ingot casting is a process where molten steel is poured into ingot molds for solidification, suitable for special steel grades, forging ingots, and large-section products difficult to produce by continuous casting.
Ingot Mold Parameters
| Parameter | Typical Range |
|---|
| Ingot Weight | 8-20 t |
| Height/Width Ratio | 2.5-3.5 |
| Taper | 0.8-4.2% |
| Wall Thickness | 50-160 mm |
| Mold/Ingot Weight Ratio | 0.8-1.2 |
| Corner Radius | 8-15% of diameter |
Taper Calculation Formula:
- Square Section: Taper = (D₁ - D₂) / H × 100%
- Round Section: Taper = (R₁ - R₂) / H × 100%
D₁ and D₂ are the lengths of the top and bottom edges, R₁ and R₂ are the radii of the top and bottom edges, and H is the height of the ingot
| Project | Requirement |
|---|
| Preheating Before Use | 80-120℃ |
| Hoisting Requirements | Must hang four lifting lugs, return flat after turning |
| Placement Requirements | Hang double slings, align with nozzle brick and lower slowly |
| Mold Standing | Ensure ground level, 4" and 6" molds cannot stand alone |
| Damage Repair | Welding patching or mixed refractory repair |
| Scrap Standard | Promptly scrap when unrepairable |